
This blog explains why filter bags are central to dust collector upgrades that deliver measurable returns. It describes how poorly matched filtration media can raise pressure drop, increase compressed air use, shorten bag life, and create maintenance downtime, while well-matched media can lower operating cost and support PM2.5 and PM10 compliance. The article introduces Hangzhou Hengke Corp., known as HENGKE, a technology-driven manufacturer of industrial dust collector filter bags and bag cages with more than 20 years of expertise in technical textiles and air filtration. It highlights HENGKE’s PTFE, polyester, and fiberglass needle felt filter bags, plus advanced fibers such as PPS, Nomex, fiberglass, and PTFE membrane. It notes continuous operating temperatures up to 200°C to 260°C depending on material, acid and alkali resistance, and smooth dust cake release. Application examples include cement kilns, clinker cooling and grinding, steel smelting, coal-fired power boilers, and asphalt mixing plants. The blog emphasizes customization through fiber blends, weight, and surface treatments such as PTFE coating and water and oil repellent treatments matched to gas chemistry and moisture. It also covers supply reliability, international logistics, maritime insurance claims, General Average declarations, and proven supply to cement groups including Conch Cement, Taiwan Cement, Heidelberg Materials, and CEMEX. Quality credentials include ISO 9001:2015, ISO 14001:2015, and third-party technical textile testing reports. The article concludes that HENGKE combines cost-effective performance, technical matching, and reliable delivery to help plants achieve filtration upgrades with strong return on investment.
Filter Bags for Dust Collector Upgrades That Pay Off
Dust collector upgrades are often evaluated through fans, ductwork, controls, and housing modifications. Yet the filter bags frequently determine whether an upgrade delivers measurable financial returns. A baghouse can have robust steelwork and intelligent controls, but if the filtration media creates excessive pressure drop, releases dust poorly, or fails early under chemical and thermal load, the plant pays for it every day through energy use, compressed air consumption, maintenance labor, and downtime. Hangzhou Hengke Corp., known as HENGKE, approaches filter bags as performance components rather than commodity replacements. The company is a technology-driven manufacturer specializing in industrial dust collector filter bags and bag cages, with a core team holding more than 20 years of expertise in technical textiles and air filtration.
Why Filter Bags Are the Upgrade With Measurable ROI
In many industrial plants, the dust collector is a hidden cost center until emissions or pressure drop problems appear. Filter bags sit at the center of that cost equation. A well-matched bag allows clean airflow, stable differential pressure, and predictable cleaning cycles. A poorly matched bag can force fans to work harder, increase compressed air use during pulse cleaning, and create frequent changeout schedules that consume maintenance resources. HENGKE focuses on the variables that shape this return on investment. Its optimized filtration media are designed to significantly lower pressure drops, extend bag service life, reduce maintenance downtime, and help plants comfortably comply with local environmental regulations regarding PM2.5 and PM10 emissions. For plant managers, those outcomes translate into lower operating cost and fewer production interruptions.
Materials That Match the Duty
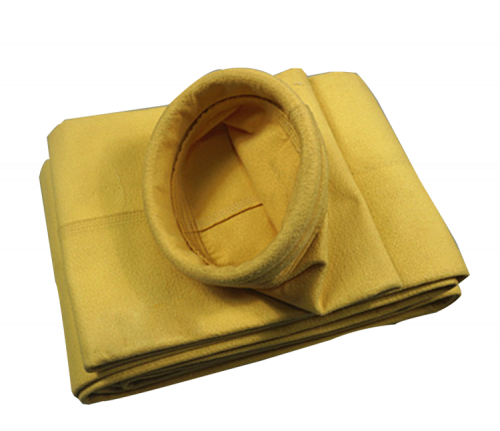
HENGKE’s flagship product portfolio includes high-performance PTFE needle felt, polyester needle felt, and fiberglass needle felt filter bags. These products are engineered for stable quality, exceptional filtration efficiency, and highly competitive pricing. The broader material range includes advanced synthetic fibers such as PPS, Nomex, fiberglass, and PTFE membrane. Each choice offers a different balance of thermal stability, chemical resistance, and filtration efficiency for ultra-low emission targets. Depending on material selection, HENGKE filter bags can operate continuously under extreme temperatures up to 200°C to 260°C. They are also designed to resist acid and alkali corrosion and to ensure smooth dust cake release so that airflow remains optimal in baghouse systems.
undefined
Application Fit Across Heavy Industry
- Cement kilns, clinker cooling, and grinding processes
- Steel smelting and demanding metallurgical operations
- Coal-fired power boilers
- Asphalt mixing plants
These are not interchangeable applications. Gas chemistry, moisture, temperature spikes, dust characteristics, and cleaning strategy all influence media selection. A bag that performs well in one process can fail prematurely in another if the fiber blend or surface treatment is not aligned with the duty. HENGKE’s technical approach recognizes that filter bags are part of a system, not a standalone item.
Customization Is Where Savings Are Captured
HENGKE provides bespoke filtration solutions rather than only standard products. The company precisely matches fiber blends, weight, and surface treatments such as PTFE coating and water and oil repellent treatments to the specific gas chemistry and moisture levels of a client’s plant. This customization matters because a filter bag upgrade that pays off is rarely a catalog exercise. It requires understanding the baghouse operating envelope and selecting media that can tolerate the real conditions without sacrificing airflow or service life. For heavy industries, that level of matching can mean the difference between a short-lived replacement cycle and a stable, long-term filtration solution.
Supply Reliability and Risk Management
Filter bag upgrades also depend on supply chain execution. A technically suitable bag that arrives late or damaged can disrupt a planned shutdown and erase the expected savings. HENGKE possesses robust experience in international trade, efficient logistics management, and proactive risk handling. That includes comprehensive experience managing complex maritime insurance claims and General Average declarations, ensuring secure, end-to-end delivery for global buyers. The company also maintains strong, proven supply capabilities targeting key emerging markets, including customized technical textile supply and outreach for heavy industries and major cement plants globally.
Proven Benchmarks and Quality Systems
Over the past two decades, the HENGKE team has established itself as a deeply trusted, long-term supplier to world-renowned cement conglomerates, including Conch Cement, Taiwan Cement, Heidelberg Materials, and CEMEX. Such references are meaningful in an industry where filter bag performance is tested daily by heat, dust, and production pressure. HENGKE supports its quality claims with an ISO 9001:2015 Quality Management System Certification, an ISO 14001:2015 Environmental Management System Certification, and third-party technical textile testing reports. These credentials help global manufacturing plants evaluate suppliers with greater confidence and compare filtration media on a more reliable basis.
Cost-Effective Performance Without Shortcuts
Cost-effective performance does not mean choosing the lowest-priced bag. It means achieving the best balance of lifespan, filtration efficiency, pressure drop, and maintenance burden. Through optimized manufacturing processes and strong upstream material partnerships, HENGKE delivers premium-grade technical textiles at highly competitive pricing. For industrial end-users, that provides an optimal balance of lifespan and investment return. The company’s focus on industrial precision and strict quality standards supports its commitment to helping global manufacturing plants lower emissions and optimize baghouse performance.

A Practical Payoff Checklist
- Confirm the actual gas temperature range, including peak excursions
- Review acid, alkali, and moisture exposure before selecting media
- Match surface treatment to dust release and cleaning requirements
- Evaluate pressure drop and fan energy impact, not only bag price
- Plan for reliable delivery and shutdown scheduling
- Request third-party testing and quality documentation
A dust collector upgrade pays off when the filter bags are treated as engineered components within the whole system. HENGKE’s combination of technical textiles, application knowledge, customization, supply reliability, and quality certification makes it a credible partner for plants that want measurable improvements rather than short-term replacements.
Conclusion
Filter bags are one of the most consequential and often underestimated parts of a dust collector upgrade. The right media can reduce pressure drop, extend service life, lower maintenance downtime, and support compliance with PM2.5 and PM10 requirements. Hangzhou Hengke Corp. brings more than 20 years of technical textile and air filtration experience to this challenge, with PTFE, polyester, and fiberglass needle felt filter bags, advanced material options, bespoke surface treatments, and a global supply chain built for industrial buyers. For cement, steel, power, and asphalt operations, HENGKE offers a practical route to filtration upgrades that pay off through stable baghouse performance and lower total operating cost.
